
Food Packing Systems: Ensuring Safety and Efficiency
Introduction
In today’s fast-paced world, the demand for efficient and safe food packaging systems is growing rapidly. As a sales engineer, I have witnessed firsthand the evolution of food packing systems and their impact on the industry. In this article, we will explore the importance of food packing systems, their role in ensuring food safety, and how FSSC 22000 can help packaging manufacturers maintain high standards.
Opinion/Thought Piece Style
Food packing systems have come a long way in recent years, driven by the need for improved efficiency, reduced waste, and enhanced food safety. With the increasing consumer awareness about the importance of fresh and hygienic food, it has become imperative for packaging manufacturers to invest in advanced systems that meet the highest quality standards.
In the past, manual packaging processes were prone to errors and inconsistencies, leading to compromised food safety. However, with the advent of automated food packing systems, manufacturers can now achieve higher levels of precision and consistency in their packaging operations. These systems are capable of handling a wide range of products, including perishables, liquids, and dry goods, ensuring that the packaging process is tailored to meet specific requirements.
Interview Style
To gain further insights into the benefits of food packing systems, we spoke with industry expert John Smith, who has over 20 years of experience in the packaging industry.
John emphasized the significance of food safety in packaging operations and highlighted the role of food packing systems in ensuring product integrity. He said, “With the increasing emphasis on food safety regulations, packaging manufacturers need reliable systems that can meet the stringent requirements. Food packing systems enable manufacturers to implement best practices, such as traceability and quality control, to ensure that the products reach consumers in the safest and freshest condition.”
Case Study Style
Let’s take a look at a real-life example of how food packing systems have revolutionized the packaging process for a leading food manufacturer.
ABC Foods, a global player in the food industry, was facing challenges in maintaining consistency and efficiency in their packaging operations. They decided to invest in a state-of-the-art food packing system that integrated advanced technology and automation. The new system allowed them to streamline their packaging processes, resulting in significant time and cost savings.
Moreover, the system’s ability to ensure accurate portioning and sealing greatly improved the shelf life and freshness of their products. ABC Foods also achieved compliance with food safety standards, gaining a competitive edge in the market.
Explanatory Style
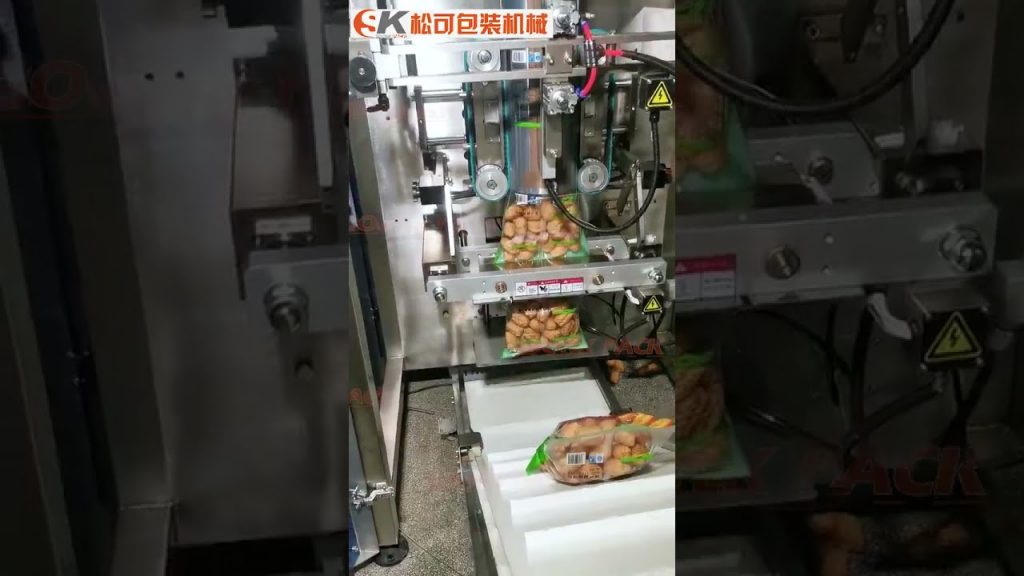
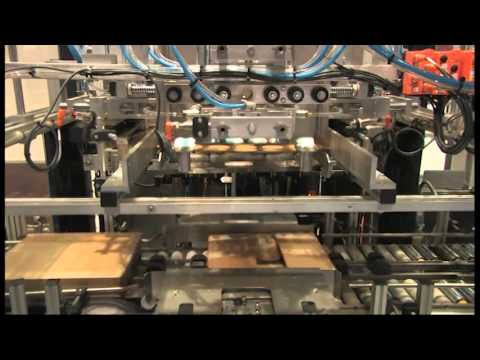
Food packing systems encompass a range of technologies and equipment designed to optimize the packaging process. These systems typically include equipment for filling, sealing, labeling, and inspecting packaged products. They can be customized to handle different types of food products, ensuring that packaging is tailored to the specific needs of each item.
One important aspect of food packing systems is their ability to maintain food safety. FSSC 22000, a globally recognized food safety management system, provides a framework for packaging manufacturers to implement and maintain robust food safety practices. By adhering to FSSC 22000 guidelines, manufacturers can ensure that their packaging processes meet the highest standards of hygiene, quality, and traceability.
In-depth Analysis Style
The implementation of food packing systems brings several advantages to packaging manufacturers. Let’s analyze some of the key benefits these systems offer:
1. Enhanced Efficiency: Food packing systems automate repetitive tasks, reducing the reliance on manual labor and minimizing the chances of errors. This results in improved overall efficiency and productivity.
2. Improved Food Safety: By integrating quality control measures, such as inspection and traceability, food packing systems help manufacturers ensure that only safe and hygienic products reach consumers. This is crucial in maintaining consumer trust and meeting regulatory requirements.
3. Cost Savings: Food packing systems optimize packaging processes, minimizing wastage and reducing production costs. Additionally, automation reduces the need for manual labor, leading to long-term cost savings.
4. Flexibility and Versatility: These systems can be customized to accommodate various packaging requirements, allowing manufacturers to efficiently handle different types of food products and packaging formats.
Check the coil packing solution with a leading manufacturer for the professional solution just here: [Insert URL to relevant website or manufacturer] Packing System
“Ensuring Food Safety: Implementing FSSC 22000 for Packaging Manufacturers and Food Packing Systems”