
Title: “Ultimate Guide to Handling Machine Manufacturers and Material Handling Equipment”
Description:
Introduction:
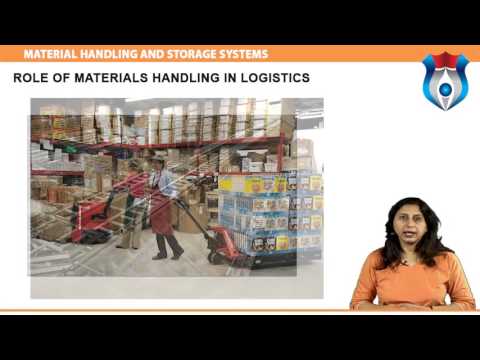
Welcome to our comprehensive guide on handling machine manufacturers and material handling equipment. In this video, we will provide you with a wealth of information and insights about handling machines, material handling equipment, and various related systems such as trolleys, pallets, bins, and steel packaging systems. Whether you are a professional in the industry or someone interested in learning more about these topics, this video is the ultimate resource for you.
Video Content:
In this video, we will delve into the world of handling machine manufacturers and material handling equipment. We will discuss the importance of choosing the right equipment for your specific needs, the benefits of using material handling trolleys, pallets, bins, and steel packaging systems, as well as the various types and features available in the market.
Key Highlights:
– Understanding the role of handling machine manufacturers in providing efficient and reliable equipment.
– Exploring the wide range of material handling equipment available for different industries and applications.
– Highlighting the advantages of using material handling trolleys, including increased productivity and reduced manual labor.
– Discussing the importance of utilizing pallets and bins in streamlining logistics and storage processes.
– Exploring the benefits of steel packaging systems in terms of durability and sustainability.
Operation Steps:
1. Introduction to handling machine manufacturers and their significance in the industry.
2. Overview of different types of material handling equipment and their functions.
3. Exploring the features and benefits of material handling trolleys, pallets, bins, and steel packaging systems.
4. Providing insights into how to select the right equipment for your specific needs.
5. Sharing best practices for optimizing the use of material handling equipment.
6. Demonstrating the operation steps of handling machines and related equipment.
Call to Action:
If you found this video informative and helpful, we would greatly appreciate it if you could hit the like button, subscribe to our channel for more insightful content, and share this video with others who might find it beneficial.
Additional Tags and Keywords: handling machine manufacturers, material handling equipment, material handling trolleys, pallets, bins, steel packaging systems, handling machines, logistics, storage, productivity, efficiency, industry, equipment selection, best practices.
Hashtags: #HandlingMachineManufacturers #MaterialHandlingEquipment #MaterialHandlingTrolleys #Pallets #Bins #SteelPackagingSystems #Logistics #Efficiency #Productivity
Title: Enhancing Material Handling Efficiency with Advanced Equipment Solutions
Introduction:
Efficient material handling is crucial in industries that deal with large quantities of goods and materials. To streamline operations, organizations are increasingly adopting advanced Material Handling Equipment (MHE) solutions. This article explores the various benefits of MHE and discusses how it can revolutionize material handling efficiency.
1. Streamlined Warehouse Operations:
MHE offers an array of equipment tailored to different warehouse needs. By utilizing automated systems, such as conveyor belts, robotic pickers, and automated guided vehicles (AGVs), companies can optimize their warehouse operations. These solutions reduce manual labor, minimize errors, and facilitate faster movement of goods, ultimately leading to improved efficiency.
2. Enhanced Safety Measures:
Safety is paramount in any material handling environment. MHE solutions prioritize employee welfare by reducing the risk of accidents and injuries. Advanced technologies, including sensors, cameras, and alarms, are integrated into MHE equipment to ensure safe operations. With enhanced safety measures, companies can minimize workplace incidents, avoid costly downtime, and improve overall productivity.
3. Increased Precision and Accuracy:
MHE equipment is designed to handle materials with precision and accuracy. Automated picking systems, such as robotic arms and automated storage and retrieval systems (AS/RS), ensure precise placement of goods, reducing the chances of errors during order fulfillment and inventory management. This accuracy leads to improved customer satisfaction, reduced returns, and minimized inventory discrepancies.
4. Efficient Space Utilization:
Limited warehouse space is a common challenge faced by many organizations. MHE addresses this issue by offering compact equipment solutions, such as vertical lift modules (VLMs) and automated mezzanines. These systems maximize vertical space utilization, enabling companies to store more materials in a smaller footprint. By optimizing space usage, organizations can reduce overhead costs and enhance overall efficiency.
5. Real-time Data Analysis:
Advanced MHE solutions are equipped with data collection and analysis capabilities. By leveraging technologies like IoT (Internet of Things) and cloud computing, companies can gather real-time data on material movement, inventory levels, and equipment performance. This data can be analyzed to identify bottlenecks, optimize workflows, and make informed decisions to further enhance efficiency.
Conclusion:
Material Handling Equipment plays a vital role in streamlining operations and enhancing efficiency. By implementing advanced MHE solutions, organizations can benefit from streamlined warehouse operations, improved safety measures, increased precision and accuracy, efficient space utilization, and real-time data analysis. Embracing these technologies will enable businesses to stay competitive in today’s fast-paced industrial landscape.Handling Machine
#Material #Handling #Equipment