
Check the coil packing solution with leading manufacturer for the professional solution just here: [Insert relevant link]
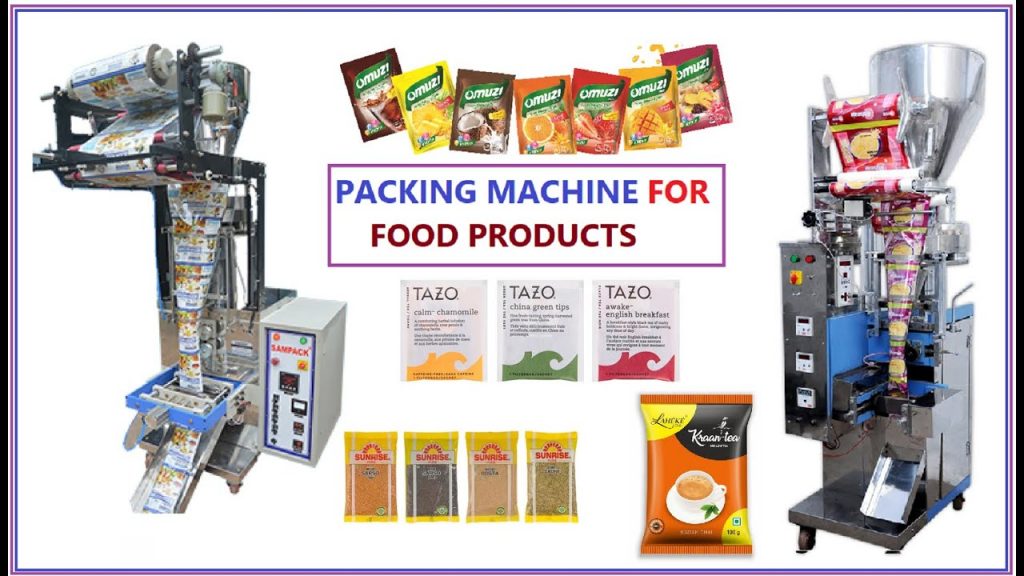
Title: Enhancing Food Quality and Shelf Life with Industrial Food Packing Machine
Introduction:
In the fast-paced world of food industry, ensuring the freshness and quality of products is crucial. One effective way to achieve this is through vacuum packaging. In this article, we will explore the benefits and functionality of the single chamber vacuum packaging machine, an essential tool for industrial food packing. We will also discuss how commercial vacuum sealers revolutionize the food packaging process.
I. Understanding the Single Chamber Vacuum Packaging Machine:
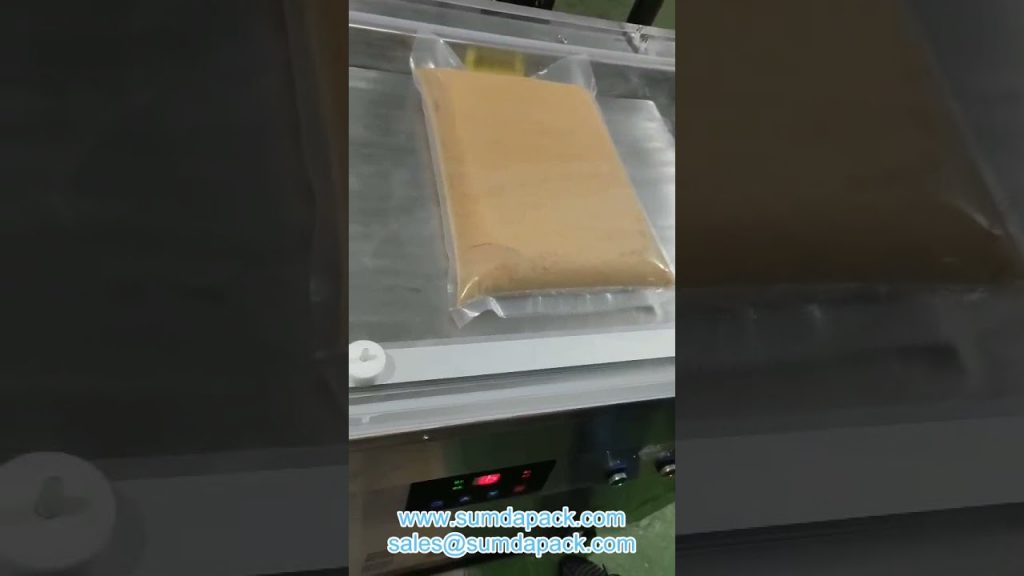
The single chamber vacuum packaging machine is a versatile equipment used for sealing food products in a vacuum-sealed environment. It is designed to remove air from the packaging, creating a tight seal that preserves the freshness, flavor, and texture of the food. This machine is widely used in the food industry for packaging various products including meat, fish, poultry, fruits, and vegetables.
II. Key Features and Benefits:
1. Enhanced Shelf Life: Vacuum packaging extends the shelf life of food by preventing the growth of bacteria and other microorganisms. By removing air and sealing the package tightly, the machine creates a barrier against external contaminants, preserving the food’s quality and freshness for a longer period.
2. Improved Food Quality: The absence of oxygen in vacuum-sealed packages helps maintain the natural color, flavor, and texture of the food. It minimizes oxidation and prevents the loss of moisture, ensuring that the food remains appetizing and appealing to consumers.
3. Cost Savings: Vacuum packaging reduces food waste by preventing spoilage. With extended shelf life, businesses can minimize product loss and optimize inventory management. This leads to significant cost savings in the long run.
4. Efficient Packaging Process: The single chamber vacuum packaging machine offers high-speed packaging capabilities, allowing businesses to achieve efficient production rates. With its automated operation, it reduces labor costs and increases overall productivity.
III. Commercial Vacuum Sealers: Revolutionizing the Food Packaging Process:
Commercial vacuum sealers have transformed the way food is packaged on an industrial scale. These advanced machines offer several advantages for businesses in the food industry:
1. Versatility: Commercial vacuum sealers can handle a wide range of food products, from solid to liquid items. This versatility makes them suitable for various food processing applications.
2. Customization Options: These machines provide customizable packaging options, allowing businesses to meet specific requirements. Different packaging sizes, shapes, and materials can be utilized, enhancing product presentation and branding.
3. Hygiene and Safety: Commercial vacuum sealers ensure hygienic packaging by minimizing the risk of contamination. The sealed packages act as a protective barrier, safeguarding the food from external factors that can compromise its safety.
IV. Conclusion:
Industrial food packing machines, specifically the single chamber vacuum packaging machine, play a vital role in extending the shelf life and maintaining the quality of food products. With their efficient operation and superior packaging capabilities, businesses in the food industry can enhance their productivity, reduce waste, and deliver fresh and appealing products to consumers.
By investing in advanced commercial vacuum sealers, food businesses can take their packaging process to the next level, ensuring the safety, freshness, and quality of their products. Stay ahead in the competitive market by harnessing the benefits of industrial food packing machines.
Check the coil packing solution with leading manufacturer for the professional solution just here: [Insert relevant link] Food Packing Machine
“Efficient Vacuum Sealers for Commercial and Industrial Food Packaging | Single Chamber Packing Machines”